Vocabulary
The followings are the important vocabulary for API 510 course explained in simple language. It not only helps you understand a few basic concepts, but some of these key words and their meaning may also be used as exam questions. Please note that the list in not exhaustive but it intends to explain important key words, their concepts and differences.
Order of Precedence
In case of conflict between reference documents such as code, recommended practice, standard, project specification, procedure, purchase order, etc., there shall be an order of precedence when one document over rules or vetoes another reference document.
For example, API RP 510 is the governing document that overrides even ASME Sec VIII for in-service pressure vessels.
API RP 510 cannot be in conflict with any prevailing regulatory requirement or jurisdictional regulation or government regulation unless it is more stringent than them.
Obviously, if API RP 510 is more stringent or more onerous than a regulation, this means, it is not in conflict with a regulation but is over and above that regulation.
Difference between Repair and Alteration
Repair means the work necessary to restore the vessel that can be operated safely at its original operating pressure and temperature.
Alteration means repairing the vessel such that it changes it’s original operating pressure and/or temperature range (integrity operating window).
So, any repair such as replacement of parts with same or similar parts (like for like) and any restoration work are called a ‘’repair’’ as long as it’s current allowable operating pressure and temperature (Maximum allowable working pressure (MAWP) and minimum design metal temperature (MDMT) does not change.
On the other hand, any activity that changes any of these parameters (MAWP, MDMT, IOW), it is termed as alteration.
Repair needs approval of the inspector while alteration needs the approval of both the engineer and inspector.
Repair examples are:
duplicate or like for like replacement.
addition of any reinforced nozzles less than or equal to the size of existing reinforced nozzles and addition of nozzles not requiring reinforcement;
also, any welding, cutting, grinding on pressure containing component that does not change MDMT or MAWP.
Alteration examples are:
Any restorative work that results to a change in MAWP, MDMT and subsequent rerating.
Rerating may be either upgrading (increase in allowable MAWP and decrease in MDMT) or downgrading (decrease in MAWP or increase in MDMT).
If re-rating leads to downgrading, then it is called de-rating which means demoting.
Please note that an increase in MAWP is an upgrade because the vessel can tolerate higher working pressure like a car that can go at a higher speed which is understandable.
But a decrease (and not an increase) in MDMT is an upgrade because the lower the MDMT, the larger, the operating window.
For example, a vessel that can operate at 10 F is superior and more versatile than a vessel that operates at 20 F.
Remember, both rerating and de-rating results in a change in MDMT and/or MAWP and hence it is termed as an alteration and not a repair.
Alteration requires a pressure test unless exempted in writing by both the engineer and inspector.
Repair does not normally require a pressure test unless specifically asked by the inspector or engineer.
Examination specifically means QC activities such as an NDT activity. It is not an inspection.
The closest analogy could be the difference between a laboratory blood test (examination) and doctor’s diagnosis (Inspection which includes evaluation and interpretation or acceptance/rejection). Examination reports shall be approved by the inspector.
NDT technician examines the material by an NDT method and reports the result.
NDT examiner can also report the acceptance or rejection of a material or equipment against an approved acceptance criteria if authorized by the inspector.
In any event, it is the inspector who shall approve the examination report.
Please remember that the inspector is the final authority in accepting or rejecting the QC and NDT examination reports.
External inspection
is the visual inspection from outside the vessel (maximum interval 5 years).
On stream inspection
On stream inspection means external inspection of vessel using an NDT technique.
The difference between external inspection and on-stream inspection is that in external inspection, only visual inspection is carried out while on-service inspection involves the NDT examination as well.
Also, external inspection is aimed at detecting the environmental corrosion while on-stream inspection is aimed at substituting internal inspection, that is, when it is possible to get the same necessary information and examination by on-stream inspection without opening the vessel up for internal inspection.
On-Stream or In- service inspection could replace periodic internal inspection if approved by the inspector and owner, provided it gives the same required information as internal inspection.
External inspection could not replace internal inspection while On Stream Inspection can replace internal inspection subject to terms and conditions.
Internal Inspection
Inspection from inside of vessel both visually and with NDT methods with a maximum interval of 10 years or half corrosion life which ever happens sooner.
Precision and accuracy are often used interchangeably, but in science they have very different meanings. Measurements that are close to the known value are said to be accurate, whereas measurements that are close to each other are said to be precise.
Accuracy is used for calibration purpose to determine how accurate the readings are with respect to a known value.
Precision shows variations. How close are a bunch of thickness measurement readings at a point on the vessel?
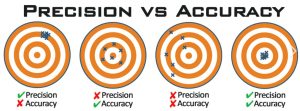
The point of measurement normally means a circular area with a diameter of 3’’.
API does not differentiate between owner and user. The owner/user is responsible for inspection and repair to meet the code.
This makes sense because if owner and user were differentiated as two separate legal entities, then, none of them could be hold them accountable because the owner would say that the user was supposed to comply with jurisdictional requirements while the user would argue that that the pressure vessel belongs to owner who should be held accountable.
Owner/user is accountable for any shortcoming and non compliance to codes and specifications or jurisdictional requirements.
API 510 requires that an owner/user shall employ or subcontract an inspection organization (or an inspection program and authorized inspector), a repair organization, an engineer, and examiner. Please note that the ultimate responsibility lies with the owner/user while other individuals are accountable to the owner/user within their scope of responsibilities.
Inspector means authorized API 510 pressure vessel inspector.
The inspector is responsible to the owner for inspection and approval of the vessel for continued safe operation.
The inspector can be an individual working for the government/jurisdiction, an insurance company, for a third party under contract with the owner/user or directly working for the owner/user.
The NDT examiner is responsible for performing NDT activities as per approved procedure and if authorized by the inspector, can also prepare the acceptance and rejection part of the report.
However, please note that the Inspector is the final authority in accepting or rejecting the NDT reports as well as all the inspection records.
Certification of the NDT examiner shall be maintained by his/her employer and shall be available for inspector’s review.
Engineer
The pressure vessel engineer is an individual or a team who is knowledgeable in the design, review, analysis and evaluation of pressure vessels and is appointed by the owner/user.
Both the engineer and the inspector shall approve any re-rating, de-rating and alteration; however, the repairs do not normally need engineer’s approval unless the inspector opt to consult with the engineer.
Corrosion Specialist
An individual knowledgeable in materials, metallurgy, damage mechanism and corrosion monitoring techniques and is approved by the owner.
Integrity Operating Window (IOW)
This is the pressure range and temperature range that the pressure vessel is allowed to work. The range is determined by design premises and depends on the type of material and its thickness.
Exceeding the IOW range may affect the integrity of the vessel. There could be other parameters within IOW such as process fluid, velocity, but MAWP and MDMT are the most prominent.
Management of Change (MOC)
Any change in the process equipment or material or hardware shall be documented. It shall be determined whether such changes may affect vessel integrity (say, by increasing the corrosion rate or change in damage mechanism).
Relevant personnel such as the Engineer, corrosion specialist, inspector, examiner and maintenance personnel may be involved to cascade down or reflect such changes in inspection planning, repair and maintenance.
Condition monitoring locations (CML)
Points or areas on the pressure vessel are identified that normally expect to have the highest corrosion rate or stress concentration. These areas are inspected and examined periodically to assess the vessel condition.
The CML locations are selected to be representative of corrosion behavior of the vessel. It makes sense to select those points or areas where maximum corrosion or damage is expected.
The inspector selects the monitoring locations based on previous history of inspection, damages occurred on similar vessels under similar operating and environmental conditions and may seek corrosion specialist opinion on expected damage mechanisms for a particular vessel.
QA & QC
Quality assurance is the design and planning of quality control activities to ensure that the service or equipment has met certain requirements while the Quality Control is the implementation of those control activities in order to demonstrate or verify that the requirements are met.
Risk-based inspection (RBI)
Not all parts or components of the pressure vessel have equal value or effect on the integrity of equipment. Similarly, not all equipment has equal value or effect on the integrity of a plant.
It is also important to understand what the consequence of failure for a particular part or equipment would be.
Risk-based inspection considers both the probability of failure and consequence of failure.
Once, we know what the probability and consequence of failure are, inspection efforts can be directed towards more critical parts, locations, parts and equipment thereby reducing the probability of failure, downtime and inspection costs while increasing equipment reliability, equipment availability and safety.
There might be a situation when the probability of failure is low, but the consequences of failure are huge and catastrophic in terms of cost, downtime or even human lives. In such situations, the overall risk is still high.
Risk = Probability of Failure X Consequence of Failure.
Quality assurance (QA) Manual
Remember that the owner/user is ultimately responsible for preparing, documenting, executing, and assessing pressure vessel/pressure-relieving device inspection and repair.
Owner/User shall have QA system that shall include:
Organization chart;
QC and QA procedures;
Report and records;
Inspection plan;
RBI assessment;
Determination of inspection interval;
Auditing;
Drawings;
Calculations;
Repair, rerating;
Management of changes;
Compliance with codes and specifications;
Record of qualified welders;
NDE technicians and WPS;
Training;
Material traceability and material certificates.
As you can see, this is more or less, a list of ISO 9001 requirements.
Temper Embrittlement
Reduction in toughness when 2 ¼ Cr 1 Mo low alloy steel exposed to high temperature range of 650 F-1100 F.
Remember that embrittlement is the reverse of ductility.
Toughness is the resistance of the material to deform under force/stress.
Toughness is quantitatively the area under the stress strain curve.
Toughness depends both on amount of stress it can tolerate, and it’s amount of elongation.
Toughness of a material is determined by Charpy impact test.
Hardness is the resistance of material against penetration or indentation.
Note: A Code document is mandatory and cannot be violated while a Recommended Practice as the name suggest, is a recommendation which means you can deviate from it based on circumstances and sound engineering practice.
Codes are based on scientific conclusions while recommended practices are mostly the result of past experience gathered over the years showing the trends and good practices.
That’s why; you may observe that most of the formulas brought within RPs are empirical. The empirical formulas have no sound scientific backing and are merely formulated to show the trends and relationship between various parameters.
Why? Because, to turn an empirical formula into a scientific formula necessitates including many more parameters of less importance and this would unnecessarily complicate the equation whereas empirical formulas are like rule of thumbs and can be of everyday use especially when you do not need to be that accurate.
The analogy would be the difference between a WPS and a Welding Instruction. The welder does not need to know about all the essential and non-essential parameters or the PQR and its associated test reports. All the welder needs to know is the range of amperage & voltage, the welding speed, the type and size of electrode, the welding position, the number of passes and if any pre heat required.
Empirical formulas are used when a very high accuracy is not important. They are basically the mathematical representation of trends.
For example, as a rule of thumb, you need to preheat 4″ or 4t from each side of the weld whichever is more. You do not really need complicated formulas to come to the right number that you cannot even implement in practice.
Scientific formulas accurately explain the phenomena for all ranges of parameters while an empirical formula only works within a limited range.
Overall, the Codes are engineering based while RPs are more experience based.